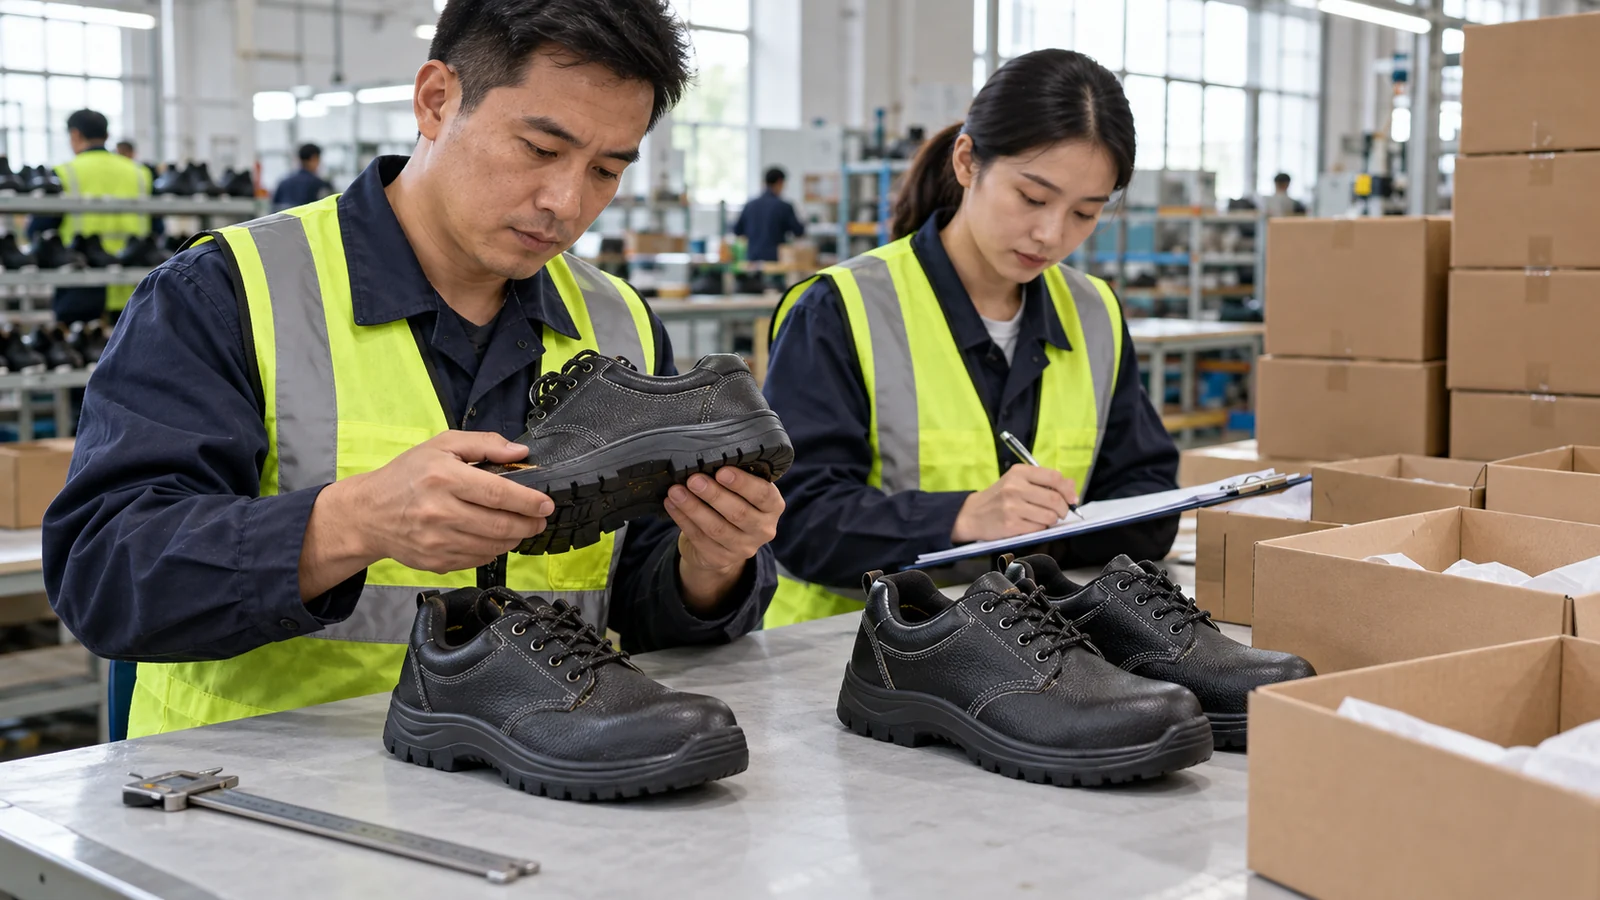
A bulk order can look correct in a few photographs while still containing mixed configurations, incorrect size assortments or packaging discrepancies. Before finished safety footwear leaves the factory, buyers need a structured way to compare the shipment with what was ordered and record unresolved findings.
This pre-shipment safety footwear inspection checklist focuses on completed goods awaiting dispatch. It helps importers, PPE distributors, wholesalers and industrial procurement managers organize checks and release decisions. It is not a substitute for laboratory testing, certification or regulatory conformity assessment, and an inspection report does not guarantee that every pair is defect-free.
1. Define the Finished Lot and Inspection Scope
Identify exactly what is being inspected: purchase order, factory location, models, production or batch references, quantities, sizes and packing status. Record whether all goods are available or whether the visit covers only part of the order. Findings from an incomplete lot should not be presented as approval of unseen goods.
Agree who performs the checks, who receives the report and who can authorize shipment. Supplier evaluation belongs earlier in the buying process; the supplier evaluation guide addresses that separate decision. At this stage, the question is whether the identified finished lot matches the agreed requirements and whether any discrepancies prevent release.
2. Assemble the Approved Specification and Reference Sample
Give the inspector a controlled reference pack: the current purchase specification, order amendments, approved sample identification, size breakdown, packaging instructions and relevant drawings or photographs. Each reference should have a recognizable version or approval date. Resolve conflicting instructions before deciding whether goods conform.
Use the pre-production sample approval checklist to understand the earlier approval record, not to repeat sample development during final inspection. A retained sample helps compare appearance and construction, but it cannot override written requirements or prove concealed components and protective performance. Record any agreed difference between the sample and the bulk specification.
3. Verify Models and Ordered Configurations
Check that selected products, their labels and their packaging refer to the ordered model and configuration. Similar-looking footwear may have different uppers, sole constructions, linings, insoles or protective components. A catalog image or shared model family is not sufficient identification.
Compare accessible features with the specification and supporting production records. Do not identify toe-cap or penetration-resistant insert materials from external appearance alone. If a configuration cannot be verified through the agreed checks and records, describe it as unverified and escalate it. Any authorized destructive examination or additional testing needs a separately defined scope, method and responsibility.
4. Agree the Sampling and Inspection Plan
Define how pairs and cartons will be selected, which models and sizes must be represented, which checks apply and how findings will be assessed. Make the goods accessible for selection across the identified lot rather than accepting only a convenient presentation of pairs chosen in advance.
There is no single sampling quantity, AQL, tolerance or pass rate suitable for every safety footwear order. If a recognized sampling plan is used, identify its applicable version and agreed parameters before inspection. Clarify defect classifications, treatment of safety-related concerns and escalation responsibilities. A sample-based result describes the inspection performed; it is not evidence that every unit was examined.
5. Review Materials, Components and Workmanship
Compare visible upper materials, color, lining, sole pattern, fastenings and assembly with the approved references. Examine accessible stitching, seams, attachment areas and finishing for discrepancies such as loose threads, open seams, visible separation, contamination or damaged components. Record locations and photographs rather than relying on a general description such as “poor quality.”
Keep observations separate from performance conclusions. A sole's appearance does not establish slip resistance, and visible attachment quality does not establish bond strength. Where composition or protective performance needs confirmation, refer to appropriate model records or agreed tests. Do not improvise a workshop demonstration and describe it as certification evidence.
6. Check Sizes, Fit References and Pair Consistency
Compare the inspected size distribution with the ordered size run, then check correspondence between product markings, box labels and carton information. Within each selected pair, check left/right identity, marked size, model, color and visible construction consistency. Note mismatched pairs and any unexplained variation across inspected sizes.
Use only agreed measurement methods and acceptance criteria for dimensional checks. A brief try-on by an inspector cannot confirm suitability for the intended workforce. Wearer trials and size planning belong earlier in procurement; the bulk-order sizing guide covers that process. Final inspection checks consistency with those approved references, not a new fit promise.
7. Reconcile Packaging, Labels and Quantities
Check product labels, individual boxes, carton marks and packing information against the order. Review model identifiers, size descriptions, agreed branding, packing units and handling information where specified. Required market markings must be reviewed against the applicable product and destination requirements, not copied from an unrelated model.
Distinguish physically counted quantities from totals taken from documents or extrapolated from sampling. Record the method and any limits. Confirm that the packing list, carton identification and inspected goods agree, and note damaged packaging, mixed assortments or incomplete packing. Do not describe an unchecked carton count as a verified pair count.
8. Review Documentation and Traceability
Connect the inspection report to the lot, purchase order, model/configuration references, inspected cartons and sample identifiers. Keep the photographs and findings identifiable enough that the supplier and buyer can locate affected goods without guessing.
Review the documents agreed for the order and destination, including their relationship to the actual configuration where relevant. The safety footwear standards guide explains why model-specific evidence matters. Possession of a document bearing a familiar standard or mark does not, by itself, establish that it covers the inspected goods. Missing or inconsistent evidence should be recorded and referred to the responsible reviewer.
9. Use a Practical Pre-Shipment Inspection Checklist
Adapt this table to the purchase order before the inspection. It identifies checks and records, not universal acceptance limits. For each row, record the outcome, evidence reference and any follow-up owner. Use “not checked” or “not applicable” explicitly rather than treating an empty field as approval.
| Check area | Compare or inspect | Record for the release review |
|---|---|---|
| Lot and readiness | Order, models, batch identifiers, availability and packing status | Actual scope, exclusions and unavailable goods |
| Approved references | Specification revision, amendments and reference sample | Versions used and unresolved conflicts |
| Configuration | Model, accessible components and supporting records | Verified features and unresolved configuration questions |
| Sampling | Selection method, cartons, sizes and agreed criteria | Items examined and inspection limitations |
| Workmanship | Accessible seams, attachment areas, finishing and damage | Located findings with photographs |
| Sizes and pairs | Markings, left/right pairing and agreed measurements | Mismatches and recorded measurements |
| Packing and quantity | Boxes, carton marks, assortments and packing list | Count method and discrepancies |
| Documents | Order-specific records and relevant model evidence | Missing, inconsistent or out-of-scope documents |
| Corrective action | Affected goods, containment and proposed correction | Responsible person and verification needed |
| Release | Outstanding findings and authorized decision | Hold/release status, scope and dated authorization |
10. Record Nonconformities and Corrective Actions
For each discrepancy, state the requirement, observed condition, affected sample or carton and supporting evidence. Record how many instances were found within what was examined; do not convert that observation into an unsupported estimate for the entire shipment.
Agree how affected goods will be identified and held while the finding is reviewed. The response may involve sorting, correction, replacement, further investigation or additional testing, depending on the issue. Record responsibility and the evidence needed to verify completion. A promise to correct the goods is not a completed corrective action, and revised photographs may not resolve every type of finding.
11. Document Reinspection and Shipment Release
Reinspection should address the original finding and any consequences of sorting or rework. Identify the goods available for review, work completed and checks repeated. If the lot or configuration changed, decide whether the original inspection scope remains adequate rather than assuming its result still applies.
Keep the inspector's findings distinct from the buyer's release authorization. The authorized decision-maker should review unresolved issues, document limitations and any permitted contractual deviations. A commercial concession cannot replace required safety or conformity evidence. Record a clear hold or release decision for the identified scope; silence should not be treated as authorization.
Before dispatch, confirm that approved corrections and packing-list updates relate to the goods actually being shipped. If loading or dispatch verification was outside the inspection scope, say so. Retain the report and release record with the order documents for receiving checks and any later investigation.
Pre-shipment inspection is one control within a wider purchasing process. The OEM buying guide places it within development, production and shipment planning. For finished bulk goods, the practical objective is narrower: document what was checked, identify what remains unresolved and make a traceable shipment decision without overstating what inspection proves.